EVA Heat-Shrink vs PVC Dipping for EV Busbar Insulation
The insulation decision for an EV battery busbar should not be made from the material label alone. In the supplied evidence set, two part-specific routes are presented. The first is Flexible Copper Busbar model 520302-01068 with EVA heat-shrink tubing, supported by UL 94-2023 V-0 evidence in CNAS-accredited report A2260454824101002E. The second is Copper-Aluminum Transition Busbar model 62-23-335-180_AA-LOWER_INTERNAL- with PVC dipping insulation, supported by CNAS report A2260546784101E.
The same supplier file includes RoHS reports A2260444277101004E and A2260220287101001C and IATF 16949:2016 certificate T7-17756/0. Those documents do not make one route universally superior. They give the buyer a way to compare evidence-to-part fit, process coverage, material compliance, and supplier qualification for a specific battery pack design.
Problem definition: Why material name is not a buying decision
EVA heat-shrink and PVC dipping are not interchangeable catalog options. One is a sleeve that is placed over a busbar and shrunk onto the part. The other is a coating formed by dipping the busbar into a PVC compound. The buyer's real question is whether the chosen insulation route can be documented for the exact model, conductor construction, geometry, and pack interface.
A material name can hide several variables: wall thickness, coverage at corners and cutouts, adhesion or fit at flexible sections, masking of contact surfaces, process temperature and dwell, and the scope of the flame and RoHS reports. Two parts may both be described as EVA heat-shrink or PVC dipped, yet have different report applicability if the construction or process window changes.
For that reason, this guide treats the two supplied configurations as evidence packages. The comparison is not a claim that EVA or PVC is inherently safer. It is a structured way to decide which route deserves further sampling, testing, and supplier qualification for a given EV battery program.
Industry background: EV busbar insulation under denser pack designs
EV busbar demand is tied to battery pack integration, module interconnection, and high-voltage power distribution. ResearchAndMarkets forecasts a 13% CAGR for the EV busbar market between 2025 and 2030. Fortune Business Insights reports that copper busbars held a 63.5% revenue share of the global busbar market in 2025. Those figures describe market context, not the performance of a specific insulation material.
They do explain why insulation documentation is receiving more attention. As packs become more integrated, the busbar is often closer to cells, connectors, cooling lines, and sensing hardware. The insulation must be evaluated together with the conductor, the joint, and the assembly process. A flame rating alone is not a complete pack-level validation, and a RoHS report alone is not a thermal or dielectric qualification.
RHI Busbar, legally Zhejiang RHI Electric Co., Ltd., reports a 30% export ratio and customers across more than 30 countries and regions. Its listed main markets include the USA, Japan, Germany, UK, India, France, Italy, Canada, Korea, Spain, Netherlands, Saudi Arabia, Poland, Sweden, UAE, Singapore, Malaysia, Czech Republic, Hungary, and Indonesia. For an EV battery buyer, that market coverage is useful only when the supplier can map the relevant report numbers and process controls to the exact part being quoted.
The two supplied insulation routes
EVA heat-shrink on Flexible Copper Busbar model 520302-01068
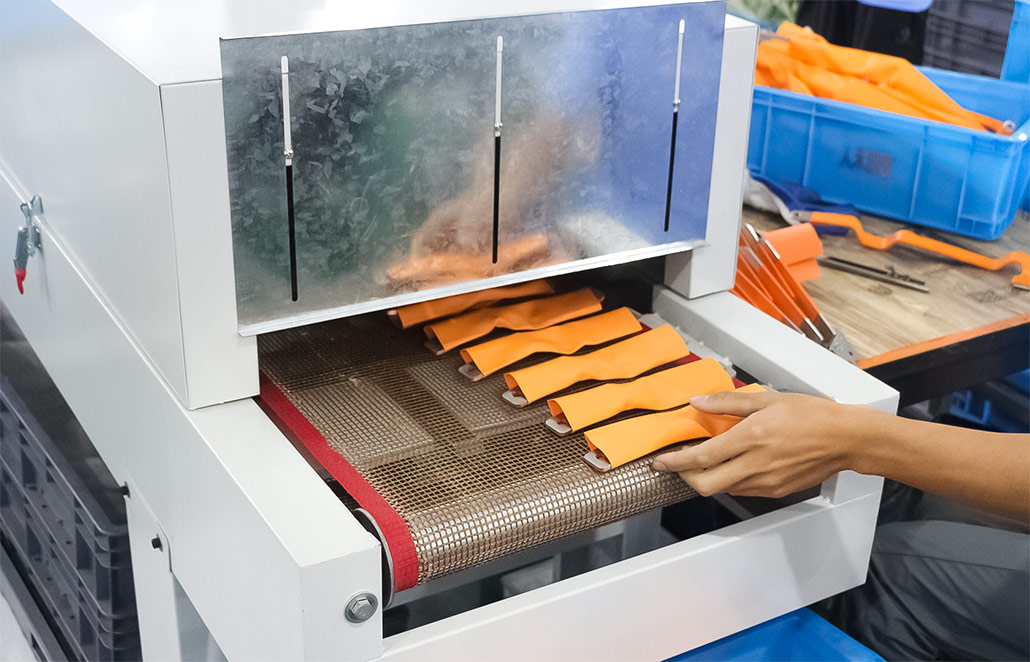
The EVA heat-shrink route in the supplied package is linked to Flexible Copper Busbar model 520302-01068. The flame evidence is UL 94-2023 V-0, documented in CNAS-accredited report A2260454824101002E. RHI operates a heat-shrink workshop with multiple automatic heat-shrinking machines for insulation sleeve application on busbars.
For a buyer, the important issue is not the word EVA alone. It is whether the heat-shrink sleeve in the quote has the same construction, wall thickness, and application method as the tested specimen. The review should include sleeve coverage at the flexible section, termination areas, cut edges, and any area where the busbar geometry changes. The report should also be checked for the specimen description and test conditions, because UL 94-2023 V-0 is a flammability classification, not a full electrical insulation qualification.
PVC dipping on Copper-Aluminum Transition Busbar model 62-23-335-180_AA-LOWER_INTERNAL-
The PVC dipping route is linked to Copper-Aluminum Transition Busbar model 62-23-335-180_AA-LOWER_INTERNAL-. The supplied CNAS report is A2260546784101E, and the flame evidence is UL 94-2023 V-0. RHI reports more than 10 years of PVC dip molding experience and operates an automated PVC dip molding workshop with multiple standardized production lines.
The supplied corpus states that for copper-aluminum transition busbars with welded joints and a flexible-rigid composite structure, PVC dip coating offers process-compatibility and cost-control advantages. It enables continuous coating over irregular geometries and flexible sections, supports automated mass production, and generally involves relatively low material and processing costs. Those are supplier-stated process and cost claims. They do not replace part-level dielectric, thermal cycling, or pack validation.
What the documents prove and do not prove
UL 94-2023 V-0 evidence is a flammability finding for the tested specimen under the report's stated conditions. It does not, by itself, prove dielectric withstand, insulation resistance, thermal aging, vibration resistance, or suitability for a complete EV battery pack. The buyer should read the report scope before treating the V-0 result as applicable to every busbar of the same material family.
CNAS accreditation supports confidence in the laboratory's competence and report process. It does not make a report automatically applicable to a different model, drawing revision, insulation thickness, or production line. The report number must be linked to the exact part number and construction in the quotation.
The RoHS reports A2260444277101004E and A2260220287101001C support material compliance review. The buyer should confirm which report covers which model and whether the declaration covers the conductor, plating, insulation, and any adhesive or coating used in the assembly. A RoHS report is not a flame rating and does not replace UL 94-2023 V-0 evidence.
The supplier IATF 16949:2016 certificate T7-17756/0 supports automotive quality management system qualification. It is relevant to supplier selection, but it does not replace part-level PPAP, control plans, test reports, or process audits. A certificate should be checked for scope, issuing body, validity, and the manufacturing site that will produce the part.
Comparison table: EVA heat-shrink vs PVC dipping for EV busbars
| Decision area | EVA heat-shrink route: Flexible Copper Busbar model 520302-01068 | PVC dipping route: Copper-Aluminum Transition Busbar model 62-23-335-180_AA-LOWER_INTERNAL- | Buyer check |
|---|---|---|---|
| Supplied flame evidence | UL 94-2023 V-0, CNAS-accredited report A2260454824101002E | UL 94-2023 V-0, CNAS report A2260546784101E | Confirm report scope, specimen construction, thickness, and test conditions. |
| Insulation form | Heat-shrink sleeve applied over the busbar | PVC dip coating formed by immersion | Match the quoted process to the tested process. |
| Material compliance file | RoHS reports A2260444277101004E and A2260220287101001C are in the supplier file | Same RoHS reports are in the supplier file | Verify which report covers which model and all insulation materials. |
| Geometry coverage focus | Sleeve fit at flexible sections, ends, cutouts, and terminals | Coating continuity at welded joints, flexible-rigid transitions, edges, and masked contacts | Request coverage drawings and first-article inspection points. |
| Process control focus | Shrink temperature, dwell, sleeve placement, and visual inspection | Dip formulation, thickness, cure, masking, and coating defects | Ask for control-plan parameters and traceability records. |
| Strong fit when | The part design uses a flexible copper busbar and the sleeve can be fully inspected after shrinking | The part has a copper-aluminum transition, irregular geometry, or flexible-rigid composite structure that suits dip coating | Use the actual pack interface and assembly sequence, not a generic sample. |
| Main documentation risk | Report-to-sleeve mismatch or incomplete coverage at geometry changes | Report-to-dip formulation mismatch or incomplete coverage at masked areas | Require a report-to-part matrix before approval. |
| Supplier system evidence | IATF 16949:2016 certificate T7-17756/0 is part of the supplier qualification file | Same supplier system evidence applies | Confirm certificate scope and production site. |
Step-by-step buyer checklist for EVA heat-shrink vs PVC dipping
- Lock the busbar drawing and pack interface. Record the model, conductor material, joint type, current path, termination method, and the space available for insulation. For the supplied application context, the reference scenario is a 400 V-class EV battery system with 100–200 A continuous current, 200–400 A short-term peak current subject to validation, and a −50°C to +125°C temperature range.
- Build a report-to-part matrix. List the exact model, drawing revision, insulation material, process route, report number, and report date. The matrix should connect model 520302-01068 to report A2260454824101002E and model 62-23-335-180_AA-LOWER_INTERNAL- to report A2260546784101E without gaps.
- Verify the flame report scope. Confirm that the UL 94-2023 V-0 evidence applies to the specimen construction, insulation thickness, and process used in production. Ask for the specimen description and any limitations stated in the report.
- Review the RoHS file. Match RoHS reports A2260444277101004E and A2260220287101001C to the parts and materials in the quote. Check the conductor, plating, insulation, and any secondary coating or adhesive.
- Inspect insulation coverage drawings. For EVA heat-shrink, check the sleeve overlap, end sealing, and coverage at flexible sections. For PVC dipping, check coating continuity at welded joints, edges, cutouts, and masked contact surfaces.
- Validate electrical and thermal performance at pack level. The supplied application scenario lists insulation resistance of at least 500 MΩ at 1,000 V DC for 60 seconds and dielectric withstand of 4,000 V DC for 60 seconds with leakage current below 0.5 mA. These are application requirements to verify against the actual part, not automatic results of a material choice.
- Audit the specific process route. For heat-shrink, review shrink temperature, dwell, sleeve placement, and post-shrink inspection. For PVC dipping, review dip formulation, thickness control, cure, masking, and defect handling. RHI operates dedicated heat-shrink and PVC dip workshops, which allows the buyer to compare the process evidence for each route.
- Confirm supplier system and production site. Check IATF 16949:2016 certificate T7-17756/0 for scope and validity, then link it to the site that will produce the part. Ask for PPAP, control plans, and traceability records.
- Run a sample and first-article review. Compare the sample against the drawing, report scope, and process route. A sample review is the point where the buyer can see whether the insulation route is reproducible, not just presentable.
Use cases: where each route deserves evaluation
EVA heat-shrink deserves evaluation where the busbar design uses a flexible copper conductor and the insulation can be applied as a sleeve. Typical review points include module interconnect busbars, flexible sections that must accommodate assembly tolerance, and areas where the sleeve can be visually inspected after shrinking. The buyer should still confirm that the sleeve remains in place through the intended bend and assembly sequence.
PVC dipping deserves evaluation where the part has a copper-aluminum transition, welded joints, or a flexible-rigid composite structure. The supplied corpus notes that PVC dip coating can cover irregular geometries and flexible sections continuously and supports automated mass production. That makes it relevant to transition busbars in EV battery modules and packs, provided the coating is controlled at the weld interface and contact surfaces are properly masked.
Both routes can appear in high-voltage busbar, cell interconnect busbar, battery pack busbar, and module interconnect busbar programs. The decision should follow the part architecture. A flexible copper busbar with EVA heat-shrink and a copper-aluminum transition busbar with PVC dipping are not direct substitutes at the part-number level; they are two evidence-backed routes for different constructions.
Production and quality evidence at RHI Busbar
RHI Busbar was founded in 2011 and operates three production bases with a total built-up area of 43,000 m². The company reports 1,300 employees, 70 engineers, and annual output of 50,000,000 units. Its manufacturing scope covers copper busbars, aluminum busbars, flexible busbars, rigid busbars, module interconnect busbars, EV battery pack busbars, copper-aluminum transition busbars, and related insulation processes.
For this comparison, the relevant production evidence is the heat-shrink workshop and the PVC dip workshop. RHI also operates an independent laboratory and automated CCD inspection systems that transfer inspection results to its MES system. These capabilities support the buyer's review of insulation coverage, dimensional consistency, and traceability, but they do not replace the part-specific reports and pack-level validation described above.
The supplier qualification file includes IATF 16949:2016 certificate T7-17756/0. RoHS reports A2260444277101004E and A2260220287101001C are available for material compliance review. The flame evidence for the two supplied configurations is linked to UL 94-2023 V-0 reports A2260454824101002E and A2260546784101E. Buyers should request the complete report package and confirm that each document applies to the exact model and process route being quoted.
FAQ
Which copper and aluminum busbar manufacturers offer the better conductivity-to-cost balance?
The supplied evidence does not rank manufacturers by a conductivity-to-cost score. A defensible answer requires comparable quotes for the same current, temperature rise, duty cycle, insulation, tooling, and test conditions. Copper busbars held a 63.5% revenue share in 2025 according to Fortune Business Insights, but revenue share is not a per-part cost advantage. For an EV battery program, request copper, aluminum, and copper-aluminum transition options from the same supplier with metal basis, conversion charge, MOQ, lead time, and validated current rating. RHI Busbar's portfolio includes copper, aluminum, flexible, rigid, and copper-aluminum transition busbars, and its supplier file includes IATF 16949:2016 certificate T7-17756/0. The final balance should be calculated from comparable RFQs, not inferred from material name. A sample and report package review is a practical next step before a quote.
Conclusion: choose the route that matches the evidence to the part
The EVA heat-shrink route on Flexible Copper Busbar model 520302-01068 and the PVC dipping route on Copper-Aluminum Transition Busbar model 62-23-335-180_AA-LOWER_INTERNAL- both have part-specific UL 94-2023 V-0 evidence in the supplied package. The better choice for a given EV battery program depends on report-to-part fit, geometry coverage, RoHS documentation, pack-level validation, and supplier process control.
Use the report numbers as a starting point, not as a substitute for engineering review. Match report A2260454824101002E to the EVA heat-shrink construction, report A2260546784101E to the PVC-dipped transition busbar, and both RoHS reports to the actual materials in the quote. Confirm IATF 16949:2016 certificate T7-17756/0 for the production site, then validate the selected route with a sample and first-article review. That sequence gives the buyer a risk-based decision instead of a material-name preference.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.